Hey there, Mono Layer Film Blowing Machine
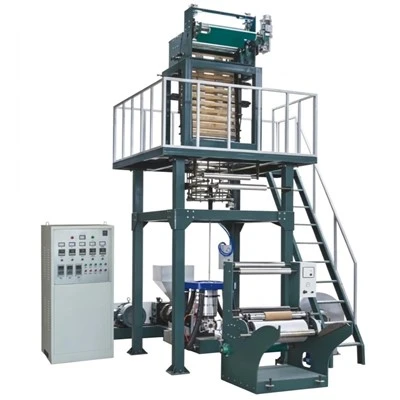
If you’re reading this, chances are you either run a small packaging shop, manage a mid-sized manufacturing line, or maybe you’re just starting out with mono layer film blowing machines—first off, welcome. I’ve been supplying these bad boys for over a decade now, and let me tell you, the number one question I get from new operators (and even some old heads) isn’t “How do I get the right film thickness?” It’s “How do I not end up with a trip to the ER, or a machine that’s down for a week because I skipped a step?”
Let’s cut to the chase: mono layer film blowing machines are pretty straightforward pieces of equipment, but they’re also powerful. You’re dealing with molten plastic at temps that’ll give you a 3rd degree burn faster than you can blink, rotating parts that’ll catch loose fabric like it’s Velcro, and high-pressure air that can send a film bubble flying across the shop if something’s off. Over the years, I’ve seen guys skip a safety check because they “just need to run a quick order” and end up out of work for months. I’ve also had a customer’s line go down for 5 days because their operator forgot to lock out the hopper before cleaning it—something totally preventable.
So today, I’m not gonna give you some generic OSHA checklist that sounds like it was written by a robot. I’m gonna break down what actually works on the floor, the little tricks I tell every new operator when they pick up a machine from us, and the mistakes I see people make again and again. Let’s get into it.
First off, pre-start checks—this isn’t “wasting time,” it’s saving your ass. I know, when you’re pressed for orders, walking through every step feels like a drag. But trust me, I once had an operator tell me “I’ve run this same machine for 2 years, I don’t need to check anything.” Three hours later, the gearbox seized because the oil level was a quart low, and they lost a $10k order. So here’s the stuff you actually need to do before you even hit the power button.
Start with the lockout/tagout (LOTO) process. Wait, no—hear me out. A lot of people think LOTO is only for maintenance, but before every start-up, you should do a quick “test” of the lock. When you shut the machine down, lock the main power source, try to turn the key—if it doesn’t move, you’re good. If it does, someone else left it on, or there’s a short. Simple, but so many skip it. Next, check the hopper. If there’s leftover plastic from the last run, don’t just pour in new resin. Old plastic can degrade, cause clogs, or even release fumes when it melts. I once had a customer’s machine emit toxic fumes because they had a chunk of old PVC left in the hopper with new PE—thankfully, someone noticed before anyone got sick, but that could’ve been way worse.
Then, the temperature gauges. Mono layer machines run at specific temps depending on the resin (LDPE, HDPE, LLDPE, whatever you’re using). Don’t just set the numbers and walk away. Let the barrel and die head hold that temp for 15-20 minutes before you start extruding. Why? Because if the die isn’t up to temp, the plastic won’t flow right—it’ll cause clogs, and when you finally push it, the pressure spikes, which can blow the die or damage the extruder. I’ve had new operators skip this, and they come back yelling “your machine is broken” when it was just them not waiting. Also, check the safety guards on the rotating parts—extruder screw, nip rolls, haul-off unit. Make sure none are bent, and they click into place when you close them. If a guard is broken, don’t tape it up—replace it. We keep spares on hand for exactly this, because a $20 guard is way cheaper than a hand injury.
Okay, now you’re ready to start the machine, but hold up—when you first start extruding, don’t crank the speed all the way up. Run it slow for 5 minutes, let the plastic flow evenly through the die, check for any leaks or lumps. Then, when you blow the bubble, start with low air pressure. A bubble that’s too big too fast can swing into the side of the machine, or the ceiling, and pop—sending molten plastic shrapnel everywhere. I’ve seen a bubble pop and hit a operator’s shoulder, leaving a burn that took months to heal. Slow and steady wins here, every time.
Now, the stuff you do when the machine is running—this is where most accidents happen, because people get complacent. Let’s talk about the zone around the extruder, die, and haul-off. Loose clothes, jewelry, long hair—if you have any of that, tie it back, take off rings, roll up your sleeves. I had an operator with long hair that wasn’t tied back get it caught in the haul-off roll. It pulled him so hard, he ended up tearing his shoulder. He was lucky it didn’t take more. Even a tiny loose thread can get caught in those rolls, so be thorough here.
Next, never reach over the die or the bubble. The die is at like 200-300 degrees Celsius—touch it, you’re getting burned. Even if you think you’re just adjusting something, use a long tool, not your hand. We supply each machine with a set of long wrenches and bubble clamps for exactly this. And if the bubble starts to wobble or get uneven, don’t panic—don’t stick your arm in to push it straight. Use the air valves on the side of the machine to adjust the air pressure in the bubble ring, or tweak the haul-off speed a little. That’s what those controls are for.
Another big one: when you need to clear a clog. Clogs happen, especially if you’re switching resin types or old plastic was left in the barrel. A lot of guys shut the machine down for 5 minutes, then try to pry the clog out with a screwdriver while it’s still warm. Don’t do that. Molten plastic is sticky, and if you jam a screwdriver in there, it can snap, fly out, and hit someone. Also, if you turn the machine back on, the screw will push that screwdriver right through the barrel. Wait until the barrel cools to a safe temp (we put a temp alarm on all our machines that beeps when it’s under 50 degrees C) before you do any manual cleaning. And even then, use a brass rod, not steel—brass won’t scratch the barrel lining, which saves you from having to replace the whole extruder later.
What about when you’re doing maintenance? Lockout/tagout is non-negotiable here. Every time you open a guard, adjust a part, or clean the inside of the machine, lock the main power, take the key with you, and post a sign that says “Maintenance in Progress—Do Not Operate.” I once had a maintenance guy leave the key in the lock, turned off, not locked. A new operator came in, didn’t see the sign, hit the start button, and almost killed the tech inside. That’s on everyone, but LOTO is the only way to prevent that. And when you’re changing the nip rolls or haul-off belts, make sure they’re locked in place before you turn the power back on. A belt that’s not seated right can fly off and hit someone, or the roll can spin and crush your hand.
Now, let’s talk about the little daily habits that keep everyone safe. First, keep the floor around the machine clean. Spilled resin, water, or film scraps are slip hazards. I’ve had more than one operator take a tumble right next to the extruder, and even a fall on concrete near hot parts is bad news. Sweep up scraps every shift, wipe up any spills as soon as they happen. Second, have a fire extinguisher nearby that’s rated for plastic fires (class B, for you guys who know the codes). Plastic fires burn hot and fast, so don’t use a regular dry extinguisher. We mount a compact one right next to every machine we sell, and we make sure operators know where it is before they run their first job. Third, never work alone. At least two people should be in the room with the machine whenever it’s running, especially for large runs or new jobs. If someone gets hurt, the other person can hit the emergency stop, call for help, or grab the first aid kit.
Wait, let’s also address something I get a lot: “Is it safe to run the machine at max speed all the time?” No, not really. While mono layer machines are built to handle consistent speeds, running them at max for hours on end can cause more vibrations, which loosen guards, wear down parts faster, and even make the bubble unstable. Not to mention, faster extruders mean hotter molten plastic, which increases burn risk. We usually recommend running at 80% of the machine’s rated speed for regular jobs, and only bumping it up if you really need to meet a tight deadline. It’s safer, and it also extends the life of your machine—win-win.
Oh, and training! I can’t stress this enough. When you get a new machine from us, we do on-site training for your operators, but even after that, refreshers every 6 months are a good idea. I’ve had customers tell me “my guys know how to run it” then I come in and see them doing things I’ve never taught, like reaching over the die or skipping LOTO. Sometimes people get complacent, so a quick refresh, a reminder of the safety rules, can prevent an accident. Also, if you have a new operator, never let them run the machine alone for the first week. Pair them with a seasoned operator who’s got the safety habits down, not just someone who can run the machine fast.
Now, let’s talk about what to do if something does go wrong, even if you followed all the rules. First, hit the emergency stop immediately—don’t hesitate. That big red button is there for a reason, use it. If you’ve got a burn, even a small one, run it under cold water for 10 minutes before going to the hospital. For cuts or crush injuries, don’t move the injured person unless they’re in immediate danger, call for emergency help right away. And if there’s a fire, get everyone out of the area before grabbing the extinguisher—don’t try to be a hero.
At the end of the day, safety isn’t just a rule—it’s about going home to your family at night. I’ve seen guys get hurt because they thought skipping a step was no big deal, and it changes everything. The good news is, operating a mono layer film blowing machine safely isn’t hard—it’s just about being consistent, not cutting corners, and respecting the equipment. We build our machines with safety in mind (guards, LOTO points, temp alarms, emergency stops everywhere), but we can’t be there every shift to remind you to do the right thing.
If you’re looking to upgrade your current machine, or you’re in the market for a new mono layer film blowing machine, we’re here to help. We don’t just sell equipment—we train your team, we keep spare parts on hand, and we’re always here if you have a safety question, even years after you buy from us. Whether you’re a small shop just starting out or a big manufacturer looking to increase safety on your line, we can hook you up. Reach out to our team to chat through your needs, get a custom quote, or ask any safety questions you have—we’re here to help you run your line safely and efficiently.
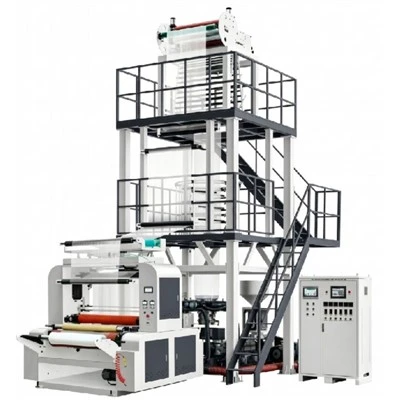
Thanks for reading, and stay safe out there.
AB Two Layer Film Blowing Machine References:
- OSHA General Industry Guidelines for Machinery and Machine Guarding (29 CFR 1910 Subpart O)
- Best Practices for Film Extrusion Safety, National Tooling and Machining Association
- Mono Layer Film Blowing Machine Operational Safety Manual, Supplier Internal Safety Standards
Ruian Jianhao Precision Machinery Co., Ltd.
As one of the most professional mono layer film blowing machine manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to wholesale durable mono layer film blowing machine for sale here from our factory. Welcome to contact us for customized service and quotation.
Address: No. 8, Jianshe Road, Beiyu Village, Shangwang Street, Ruian City, Wenzhou City, Zhejiang Province
E-mail: 1832333027@qq.com
WebSite: https://www.jianhaomachinery.com/
