Hey everyone, Carrier Tape
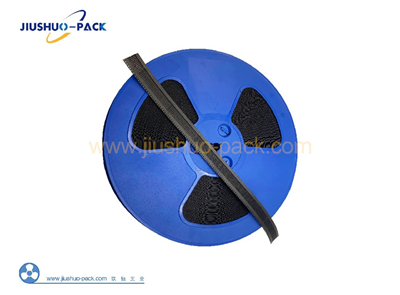
If you’re in the electronics manufacturing game, you’ve definitely seen those thin, plastic tapes with little evenly spaced pockets—carrier tapes, right? I’m not here to lecture you on random supply chain bits I copied from a textbook, though. I run a carrier tape supply company, and I’ve been talking to SMT line leads, production managers, and even the folks who pack tiny resistors for a living for years. One question pops up every single time: “How much does this little tape actually change how fast my line runs?” Today, I’m breaking that down, no stuffy jargon, just real talk from someone who’s actually around the factory floor, not just behind a computer.
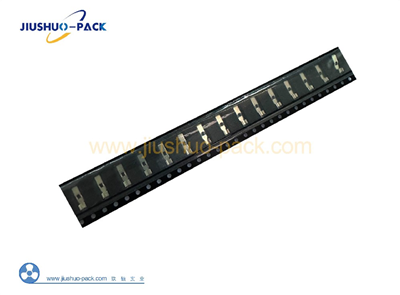
First off, let’s clear up what we’re actually talking about here, because not everyone in manufacturing mixes up carrier tapes with those shipping tapes you use to seal boxes (glad I got that out early, trust me). Carrier tape is that flexible plastic strip, usually polycarbonate or polypropylene, with pre-molded cavities (pockets) that hold tiny electronic components—think surface-mount resistors, capacitors, even microchips. You pair it with a cover tape, usually a peelable plastic or paper layer, and bingo, you’ve got a reel of components ready for pick-and-place machines. That’s the core, but the real magic (or frustration, depending on the tape) is in how that tape interacts with your line’s speed.
Let’s start with the most obvious link: bad carrier tape = slow packaging lines (or even worse, stopped lines). I remember a client a couple months back—small contract manufacturer out in Michigan, doing 0402 resistors (those tiny ones, like a grain of sand almost). They were using a cheap carrier tape from a random overseas supplier, and the pockets were molded lopsided. Every so often, a resistor would sit off-center, so when the pick-and-place arm came to grab it, it missed. I went over to their line, stood there for 20 minutes, and watched them reset the machine 12 times. At $150 an hour for that line, that’s $300 wasted in 20 minutes—not even counting the labor of the tech standing around. Fast forward a month after they switched to our tape, I got an email saying their line downtime for component feeding dropped 18%. That’s not a “marketing stat”—that’s real numbers from a factory that was hemorrhaging cash over bad tape.
Wait, but it’s not just about lopsided pockets. There’s the reel itself, too. If your carrier tape’s spool hub is too small, the tape will kink when it unwinds, right? Pick-and-place machines can’t grab components from a kinked tape—they’ll either fumble the part or jam. I had another client, a mid-sized semiconductor maker in Texas, who complained their line was stopping every 90 minutes, when it used to run 4 hours straight. Turned out, their old tape had a thin edge that stretched unevenly, so when the reel spun, the tape pulled tight and snagged. We modified the edge of our tape to have a uniform thickness, and their uptime jumped to 6 hours per reel. That’s a direct line between carrier tape quality and how efficient your packaging process is.
Now, let’s talk about component throughput, which is the big one for efficiency. Pick-and-place machines have a “feed rate” they’re rated for—usually how many components they can grab per hour. But that rate only holds if the carrier tape is optimized for the machine’s feed. Here’s a secret most suppliers won’t tell you: if your tape’s pitch (the distance between each pocket) is off by even 0.1mm, the pick-and-place arm’s camera can’t lock on fast enough. Instead of grabbing a part in 0.2 seconds, it takes 0.5 seconds. Multiply that by 10,000 parts per hour, and you’re losing 3,000 parts’ worth of time—easily cutting your line’s output by 20%. That’s not a small number. For a line churning out circuit boards that sell for $50 each, that’s $1,000 lost per hour because of a tiny tape measurement error.
We also do custom tape for parts that aren’t “standard”—like those odd-sized connectors for IoT devices. A client a while back had a new product with a 10mm x 20mm component, and every standard tape was too loose. They’d try to cram the part in, and it would shift during shipping, leading to more downtime on the line. We molded custom pockets with precision tolerances, so the part fit like a glove. Their packaging efficiency went up 25% because they didn’t have to stop and adjust the component position every time the feed advanced. That’s the thing—generic tape works for standard parts, but custom tape is where you unlock real efficiency for unique components.
Wait, I should mention cover tape too, because people sleep on this part of the carrier tape system. The cover tape is what seals the pockets, right? If it’s too tight, your operators (or machines) can’t peel it open fast enough when the pick-and-place is grabbing parts. If it’s too loose, it might peel accidentally during transport, spilling components all over the floor. A client in California had this problem: their old cover tape peeled mid-unwind, so they’d have to stop the line, clean up all the tiny parts, and replace the tape. We tested different adhesive levels on our cover tape—customized for their line’s peel speed—and their peel-related downtime dropped to almost zero. That’s another piece of the carrier tape puzzle that directly hits efficiency.
Now, let’s get into the long-term stuff, because efficiency isn’t just about the line running fast one day—it’s about consistency over weeks and months. I see a lot of clients pick the cheapest carrier tape on Alibaba or whatever, and save $0.02 per reel, but end up spending $500 a day on downtime and rework. Let’s do a quick math example, because I’m a guy who works with numbers, not just hype. Say you have 10 lines running 20 days a month, 8 hours a day. If each line has 2 hours of downtime a month because of bad tape, that’s 20 hours of lost line time per month. At $150 an hour per line, that’s $3,000 a month in lost productivity. Compare that to spending an extra $100 a month on higher-quality carrier tape—you’d save $2,900, easy. That’s the real relationship: short-term cost savings on tape lead to long-term efficiency losses, and good tape leads to consistent, long-term efficiency.
Wait, but what about when you’re packaging components for storage, not just putting them on a pick-and-place line? Even then, carrier tape impacts efficiency. If your tape has static-dissipative properties (which we build into all our tapes, by the way), you don’t have to spend extra time wrapping the reels in anti-static plastic. You can just stack them in a cabinet, pull them out, and feed them. That’s less handling, less time spent prepping components for production—another efficiency win. I had a client that used to have a whole team just prepping reels for packaging, adding extra anti-static wraps. After switching to our static-dissipative carrier tape, they cut that prep work by 40%. That’s not even on the line—that’s the back office, the prep floor, being more efficient because of the tape.
I should also address a common myth I hear all the time: “Carrier tape is a commodity. It’s all the same.” No, it’s not. Look, I’ve tested tapes from every supplier you can name, and the difference is night and day. Some tapes have sharp edges that fray when they’re fed through the machine. Some have pockets that don’t align 100% across the whole reel. Some use cheap plastic that breaks after 500 feet, leading to a whole reel of components going to waste. Those aren’t “small issues”—they’re efficiency killers. Last year, a client switched to a “generic” tape to save money, and when the tape broke mid-run, they had to throw away 3,000 parts because they couldn’t pick them from the broken tape. That’s $1,500 in parts wasted, plus the downtime to clean up. I still chuckle when I get an email from them asking for a quote for our tape, because they learned the hard way that commodity tape is not the same as quality tape.
Now, let’s talk about how we work with clients to make this even better, because it’s not just selling a tape and moving on. A lot of suppliers just dump a reel on your doorstep and call it a day. We send a rep to your line, watch your pick-and-place machine, measure your components, test a sample reel, and tweak the tape until it’s perfectly matched. For example, a client in Oregon had a pick-and-place machine that ran at 120 parts per minute, but their old tape made it only run at 95. We adjusted the pitch of our tape to match their machine’s feed timing, and now they hit 115 parts per minute. That’s a 20% speed boost, all from tweaking a tape parameter. Small changes, huge efficiency gains.
I also want to mention sustainability, because that’s tied to efficiency too. Wait, hold up—sustainability and carrier tape? Yeah. If your tape is too thick, it’s extra plastic that you have to dispose of, or extra weight for shipping. We use thin, high-grade polypropylene that’s just as strong as thicker tapes, but uses 30% less plastic. That means less waste, and lighter reels that cost less to ship. For a client that ships 1,000 reels a month, that’s a $200 savings on shipping, plus less plastic to throw away, which means less time dealing with waste management. That’s another layer of how carrier tape impacts overall efficiency—not just line speed, but the whole supply chain.
Let me wrap this up for anyone who’s still on the fence. The relationship between carrier tape and packaging efficiency isn’t vague or “nice to have”—it’s direct, measurable, and impactful. A good carrier tape cuts downtime, increases pick-and-place speed, reduces rework, cuts prep time, lowers waste, and even saves on shipping and disposal costs. A bad carrier tape? It’ll shut down your line, waste your parts, cost you money, and make your team pull their hair out.
I’m not here to push you to switch tomorrow, but if you’re tired of seeing your line stop every other hour, or if your efficiency numbers are stuck and won’t budge, we can help. I’ve seen the numbers, I’ve seen the lines speed up, I’ve seen clients stop stressing about bad tape and start hitting their production goals. No vague promises, no stuffy contracts—just real, tested carrier tape that’s built for your line, not a generic reel. If you want to chat through your specific setup, no obligation, just shoot me a message to connect. We can send samples, walk through your line, whatever you need.
Thanks for sticking with this long post—now go check that carrier tape you’re using, okay? You might be surprised how much it’s holding you back.
Plastic Reel References
- International Electronics Manufacturing Initiative (iNEMI). (2022). Surface Mount Technology (SMT) Line Efficiency Benchmarking Report.
- American Society for Quality (ASQ). (2021). Packaging Process Efficiency: The Impact of Component Feeding Materials.
- Institute of Printed Circuits (IPC). (2020). IPC-TA-600: Requirements for Tape and Reel Packaging of Surface Mount Components.
- U.S. Bureau of Labor Statistics. (2023). Manufacturing Productivity: Electronics Component Production Sector.
Dongguan Jiushuo Industrial Co., Ltd.
As one of the most professional carrier tape manufacturers and suppliers in China, we also support customized service. Please feel free to buy high quality carrier tape made in China here from our factory. Contact us for more details.
Address: 11th Floor, Building 2, Chuangfu Center, Chashan Town, Dongguan City, Guangdong Province, China
E-mail: sales06@zaidaiw.com
WebSite: https://www.carriertape-pack.com/
